
Boilermaking, forming and welding
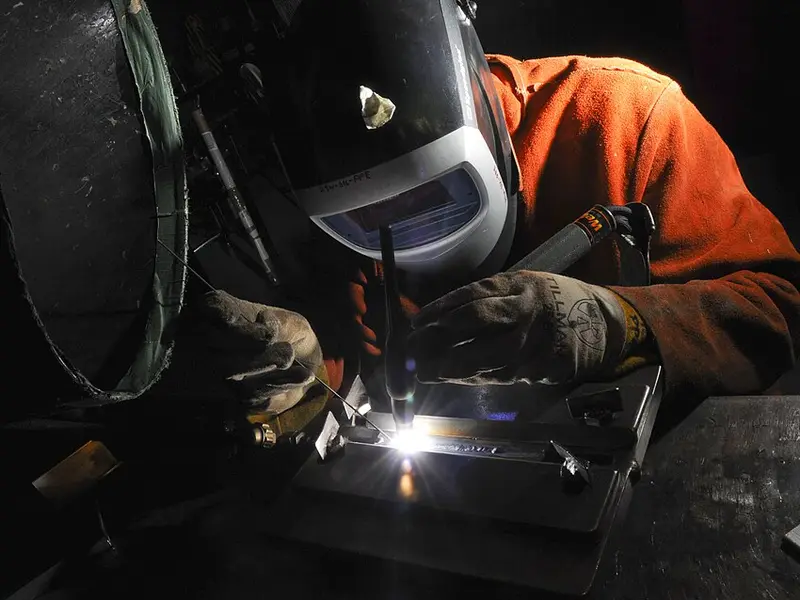
Welding: laser, TIG and MIG/MAG
We choose the process and the consumable by the alloy, the thickness and the demands of the joint. Welding special alloys requires heat input control so as not to lose corrosion resistance.
What we do
- Laser welding: narrow bead, little distortion and low heat input
- TIG (GTAW): precision joints, pipe root passes, stainless and nickel alloys
- MIG/MAG (GMAW): productivity on plates and larger parts
- Dissimilar joints (stainless to carbon steel, nickel to steel)
Materials
Capacity, maximum dimensions and lead time on request: send the drawing. See alloys in stock.
Welding processes
TIG (GTAW) uses a tungsten electrode and separate filler metal, with fine control of heat input: it is the process for pipe root passes, precision joints and nickel alloys. MIG/MAG (GMAW) feeds the wire continuously and is more productive on plates and larger parts. Laser welding concentrates the energy in a very narrow bead, with little distortion and a minimal affected zone.
The right consumable for each alloy
The filler metal does not always have the same composition as the base metal. Duplex uses a consumable with more nickel to balance ferrite and austenite; nickel alloys use more highly alloyed consumables to compensate for segregation in the bead; dissimilar joints, such as stainless to carbon steel, use consumables such as ER309L or ERNiCr-3. The filler metal catalog shows each consumable and what it is for.
Joint control
In stainless and special alloys we control heat input, interpass temperature, gas shielding (including root purging) and cleanliness. In Cr-Mo steels, preheat and post-weld heat treatment follow the design code. The weld can be verified by visual inspection, liquid penetrant and other tests as specified.
What to send with a quote request
Send the drawing of the joint or assembly, the alloys and thicknesses, the fabrication code or standard (if any), the quantity and the tests required.
More in boilermaking, forming and welding
Related services
Frequently asked questions
Which consumable for welding duplex?
Usually ER2209 for duplex 2205 and ER2594 for super duplex, which have more nickel than the base metal to balance ferrite and austenite. See the page of each consumable in the catalog.
Do you weld stainless to carbon steel?
Yes. Dissimilar joints are made with a dedicated consumable, usually ER309L or a nickel alloy when there is temperature or thermal cycling.
Does Dustre perform this service on customer-supplied material?
Yes, as long as the alloy and the specification are defined. We can also supply the material from our stock, with EN 10204 3.1 certificate.
